Hey folks, Copper Alloy Castings and Machining
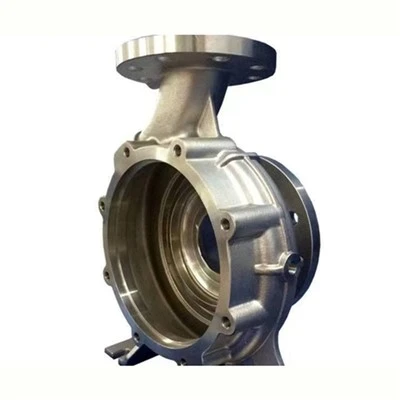
If you’re in the market for copper alloy bars—whether you’re making electrical components, heat exchangers, or heavy-duty industrial parts—chances are you’ve wondered how exactly those smooth, precise bars end up on your workbench. As a copper alloy castings and machining supplier who’s been grinding, turning, and finishing these bars for over 12 years, I’ve seen it all: from rookie machinists burning through bar stock because they didn’t account for copper’s quirks, to production lines slowing down because of wrong cutting speeds. Today, I’m breaking down what actually goes into machining copper alloy bars the right way—no fancy jargon, just the stuff we live and breathe on our shop floor.
First off, let’s get one thing straight: not all copper alloys are created equal. You can grab a random bar off the shelf and start machining, but that’s a fast track to ruined tools, wasted material, or parts that don’t fit. We work with three main types for most of our customers, and each needs a totally different game plan. Let’s run through ‘em quick:
- Free-machining copper alloys (like C36000 brass or C18400 copper chromium): These are the “easy” ones. They have small lead or bismuth bits that act like built-in lubricant while you cut, so they’re great for high-volume runs where speed matters.
- High-strength copper alloys (like C17200 beryllium copper): This is the tough stuff—used for springs, tooling, and parts that take a beating. It’s way harder than your average brass, so you can’t just crank up the spindle speed and go to town.
- Thermally conductive copper alloys (like C11000 electrolytic tough pitch copper): We use these for heat exchangers, bus bars, and electrical connections. They’re super soft, which means they can deform easily if you don’t set your feeds right.
Mistake number one we see all the time with new machinists or even small shops is ignoring that difference. Last quarter, a guy brought us a batch of C17200 bars he’d tried to machine himself with a standard high-speed steel tool—ended up chipping half his tools and wasting 30 lbs of material. That’s the kind of headache we’re here to help you avoid.
Next up: prep work that makes or breaks the whole job. You wouldn’t build a house on a lumpy foundation, right? Same with machining. First step, when we get a cast copper alloy bar (a lot of our bars start as castings, not rolled—more on that in a sec), we have to take off the “skin.” Cast bars have a thin, hard outer layer from the mold that’s way denser than the interior. If you try to cut that with a regular end mill, it’ll grab and tear the bar instead of slicing it clean. So we start with a roughing pass—usually with a carbide tool, set to a 0.1” depth of cut—to shave off that outer layer. No shortcuts here; if you skip it, your finish pass will be uneven, and the tool will wear out twice as fast.
Another prep step: securing the bar. Copper is soft, so if you clamp it too tight, you’ll leave marks or even bend the bar. Too loose, and it’ll wobble mid-cut, ruining the part. We use soft jaws on our lathes and mills—usually aluminum or brass jaws—so they grip the bar evenly without digging in. For longer bars (like 8ft ones we do for electrical bus work), we add a tailstock support too; that keeps the bar straight while it’s spinning at 500 RPM, instead of having it sag and throw off your cuts.
Now let’s get to the actual machining steps—roughing, finishing, and everything in between. Let’s start with roughing: this is where you take the bulk of material off. For free-machining alloys, we crank the spindle speed up—around 1,500 to 2,000 RPM—and set the feed rate to 0.015” per revolution. The built-in lubricant in these alloys means the chips break small and easy, so you don’t get that long, stringy mess that wraps around your tool. For high-strength alloys, we dial the speed back to 800 to 1,200 RPM, and use a harder carbide tool (we stick to solid carbide inserts for this stuff). No lead in high-strength alloys, so we have to use external coolant to keep the chips from sticking to the tool. For soft, conductive alloys, we take lighter cuts—0.008” per revolution at 1,000 RPM—because if you push too hard, the bar will deform right at the cutting edge.
Here’s a pro tip most people don’t tell you: chip evacuation. Copper chips are small, but they’re ductile, so they can clog your tool’s flutes if you don’t clear ‘em fast. We use high-pressure coolant (100 PSI minimum) aimed right at the cutting zone—sometimes we even use air blast for small parts—to blow the chips away. If you let chips build up, they’ll heat up from friction, and that heat will transfer to the bar, making it warp. We’ve had parts come back from customers because they warped after machining, and 9 times out of 10, it’s because they skipped the high-pressure coolant.
Finishing pass is where you get the smooth surface that’s ready for assembly. For free-machining alloys, we use a sharp, polished carbide tool, set to a very shallow depth—like 0.005” to 0.01”—and crank the speed up a little (2,000 to 2,500 RPM) to get that mirror-like finish. For high-strength alloys, we slow the speed to 1,000 RPM, same as roughing, but use a coated carbide insert (TiN coating works great) to reduce friction. For soft copper, we actually adjust the feed rate to be slightly faster—0.02” per revolution—at 1,500 RPM. Wait, why faster? Because soft copper will work-harden if you push too slow; that makes it harder to machine for the next pass, or if the customer has to do secondary operations. We learned that the hard way a few years back when a customer’s part came back cracked after bending—turns out we’d used a too-slow feed rate that work-hardened the C11000 bar.
Now, what about secondary operations? A lot of our customers ask about drilling, tapping, or threading copper alloy bars. Drilling copper? Use a drill bit with a 118-degree point angle—standard is 135, which is for steels. Copper cuts better with a shallower point angle, so the drill doesn’t grab the bar and pull it out of the clamp. For tapping, we use a spiral flute tap, not a straight flute—spiral taps pull the chips out of the hole instead of pushing them into the thread, which avoids broken taps and messed-up threads. And always use a tapping lubricant—mineral oil works, or we use a soluble oil for high-volume jobs. Last thing on secondary ops: deburring. Copper’s soft, so burrs form easy. We use a vibratory tumbler with ceramic media for small parts, or a nylon brush for larger bars—never a metal wire brush, that’ll scratch the surface.
Wait, let’s talk about tooling—because this is where we save our customers the most money. A lot of shops use generic tools for copper, but that’s a waste. For roughing, we use uncoated carbide inserts—they’re cheaper and work better for heavy cuts. For finishing, TiN or TiCN coated inserts cut smoother and last longer. For drills, carbide drills are a must—high-speed steel drills will wear out in half the time when drilling copper. We also change our tools after 10 to 15 passes for high-strength alloys, and 20 to 25 for free-machining—if you wait until the tool is dull, you’ll get bad surface finish and have to redo the part anyway.
And let’s not forget about casting vs. rolled bars. Some suppliers sell rolled copper alloy bars, but we use cast bars for most of our custom jobs. Why? Rolled bars are strained from the rolling process, which makes them harder to machine and more prone to warping. Cast bars are more uniform in structure, so they cut more evenly. We heat treat our cast bars after casting to relieve any internal stress, too—another step that keeps the parts from warping after machining. That’s why our customers get parts that fit perfectly every time, not ones that twist or bend a week later.
Now, let’s run through a quick example to make this real. Last month, we had a customer who needed 50 C17200 beryllium copper bars, each 2ft long, 2” diameter, with precision threads on both ends. Here’s how we did it:
- Start with cast C17200 bars, heat treated to T4 condition (relieves stress, makes machining easier).
- Roughing pass: carbide tool, 0.1” depth of cut, 1,000 RPM, 0.01” feed rate. Remove the hard outer skin, get the bar down to 2.05” diameter.
- Finishing pass: TiN coated carbide, 0.005” depth, 1,200 RPM, 0.008” feed rate, get to exactly 2” diameter.
- Drilling: 0.25” hole in one end, 118-degree carbide drill, 800 RPM, high-pressure coolant.
- Tapping: ¼”-20 thread, spiral flute tap, mineral oil lubricant, 500 RPM.
- Deburr: vibratory tumbler for 2 hours, no scratches.
- Final inspection: measure diameter, thread pitch, surface finish—all meet the customer’s specs.
Done in about 20 minutes per bar, no scrap, and the customer said they put them to use in their aerospace tooling, with zero issues. That’s the kind of result we aim for every time.
Common mistakes to avoid, so you don’t end up like that rookie guy I mentioned earlier:
- Using the wrong cutting speed/feed: Too fast, and the tool will chip. Too slow, and the copper will work-harden.
- Forgetting to remove the cast skin: That hard outer layer will destroy your tool in 1 or 2 passes.
- Skipping high-pressure coolant: Chips stick, heat builds up, parts warp.
- Clamping too tight or too loose: Marks or wobbled cuts.
- Using the same tool for roughing and finishing: Roughing tools are duller; they’ll leave a bad finish.
Now, if you’re reading this and you’re not sure if you’re doing it right, or you need custom copper alloy bars that are machined to exact specs, that’s what we do. We’re the guys that walk you through which alloy works for your project, adjust the machining parameters so you don’t waste material, and deliver parts that fit on the first try. Whether you’re a small fab shop needing 10 bars, or a big manufacturer needing 10,000, we’ve got the equipment and the know-how to get it right.
Wait, I should also mention that we don’t cut corners here. A lot of cheap suppliers will skip the heat treatment for cast bars, or use generic tools to save a buck. But that leads to customer headaches, which we hate. We’ve built our business on being the supplier that shows up when the part needs to be perfect, no excuses. If you’ve got a project that needs copper alloy bars, or you’re having trouble with your current machining process, hit us up. We’d love to chat through your needs, answer any questions, and send over a quote.
At the end of the day, machining copper alloy bars isn’t rocket science, but it does take knowing the quirks of the material. It’s all about adjusting your approach to the alloy, taking the right prep steps, and paying attention to the little stuff like chip evacuation and tooling. Skip those steps, and you’ll waste time, money, and material. Do ‘em right, and you get parts that perform exactly as they should, for whatever you’re building.
CNC Machining References:
- American Society for Metals (ASM International). (2008). Machining of Copper Alloys. ASM Handbook, Volume 16: Machining.
- Copper Development Association. (2015). Machining Guidelines for Copper and Copper Alloys. CDA Technical Report 118.
- Noria Corporation. (2022). Common Machining Errors in Copper Alloy Components. Machinery Lubrication Magazine.
Sanming Hongfeng Machinery Manufacturing Co., Ltd.
As one of the most professional copper alloy castings and machining manufacturers and suppliers in China, we’re featured by quality products and good service. Please rest assured to wholesale customized copper alloy castings and machining made in China here from our factory. Welcome to contact us for quotation.
Address: No.2 Gaoyuan Industrial Zone, Chenda Town, Sanyuan District, Sanming City, Fujian Province, China
E-mail: smhfjxzsq@163.com
WebSite: https://www.smhfmachinery.com/
